Hot Runner maintenance for a 48-cavity injection mold at a packaging manufacturer in Thailand
Customer: Multinational packaging manufacturer
We maintained injection-mold Hot Runner systems, which keep plastic molten up to the nozzle, for a packaging manufacturer in Thailand through multiple individual work orders from 2021 to 2025. We coordinated repairs with partner technicians, including short-circuited heaters, temperature controllers, manifold cleaning and nozzle housing replacement. Most jobs closed with a Service Report.
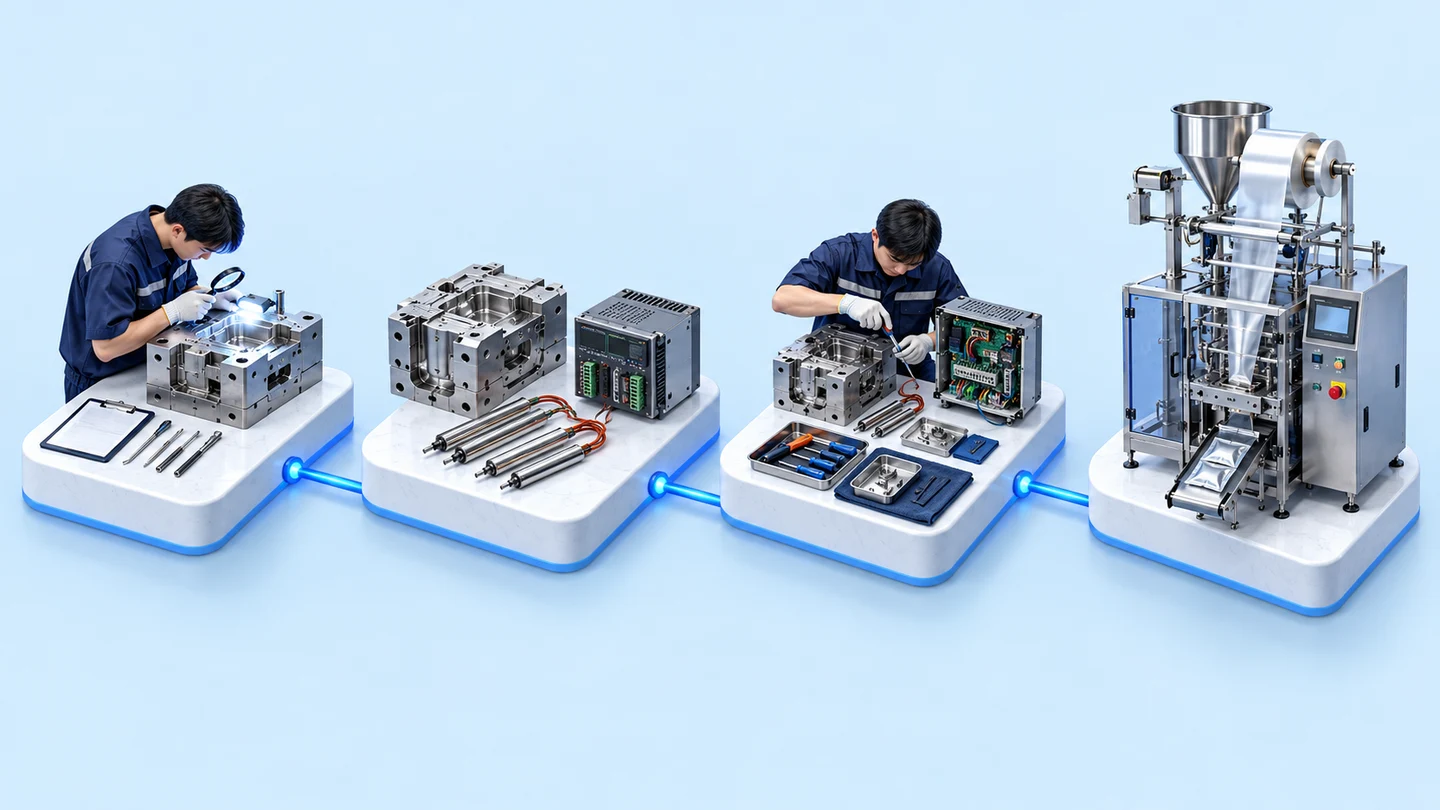
- Zone alarm / control cabinet faulte.g. Short to Ground
- Check temperature control cabinetBack Plane · MCU · wiring
- Check heaters and thermocouplesIn the mould's Hot Runner system
- Repair / replace partsor remove and clean the Manifold
- Heat-up Test + job closure documents
- Industry
- FMCG
- Year
- 2021–2025
- Scope of work
- Per-job maintenance under purchase orders, 2021–2025, for the Hot Runner systems and temperature control cabinets of several plastic injection moulds, most of them 48-cavity, both on site at the customer's factory and by taking in parts for cleaning and repair. Work with job closure documents: 2021 calibration of 6 control cabinets and replacement of Hot Runner parts · 2024 MCU board repair on a control cabinet (6-month repair warranty) and Manifold cleaning · 2024–2025 Cross Manifold repair · 2025 control cabinet Back Plane replacement, fixes to zones 26 and 44, and replacement of 48 Nozzle Housings
Summary
- This case is maintenance of Hot Runner systems on several plastic injection moulds, most of them 48-cavity, for a packaging manufacturer in Thailand, under multiple per-job work orders between 2021 and 2025.
- We coordinate repairs with partner technicians, covering both the temperature control cabinet side (calibration, MCU board repair, Back Plane replacement) and the mould side (heaters, thermocouples, Manifold and Nozzle Housing).
- Fault-fixing work traces the root cause before repair. For example, zones 26 and 44 were short-circuiting to ground because a heater wire was damaged during installation of mould parts and then touched the Manifold plate.
- In 2025, after all 48 Nozzle Housings were replaced, the mould returned to production, and the service report states that every zone could heat.
- The work on zones 26 and 44 has an acceptance document signed by the customer's representative, and most jobs have a Service Report stating the symptoms, what was fixed and the cause when one was found.
The on-site brief
The customer has several sets of plastic injection moulds, most of them 48-cavity (48 part cavities in a single mould), using a Hot Runner system whose heaters and thermocouples (temperature sensors) are divided into multiple zones. When a zone short-circuits to ground, the temperature control cabinet malfunctions or deposits build up in the runners, the mould cannot return to production until the fix is complete. The customer therefore wanted a repairer able to find the root cause on both the control cabinet side and the mould side, then test before returning the mould to the production line.
What we did
We take on work under individual purchase orders and coordinate repairs with partner technicians specialising in Hot Runner systems, both repairing at the customer's factory and taking in parts for cleaning and repair. Fault-fixing work first checks the temperature control cabinet, wiring, heaters and thermocouples, then repairs or replaces parts according to the findings.
Results
On-site repair work covered by 2025 service reports included a Heat-up Test before return, and after all 48 Nozzle Housings were replaced, the mould returned to production with every zone able to heat. The work on zones 26 and 44 has an acceptance document signed by the customer's representative. The Manifold cleaning work reported that plastic and carbon deposits were fully removed, and recommended cleaning the system every 6–12 months depending on use.
How the brief came about
The challenge in this case was to get Hot Runner plastic injection moulds back into production after problems with a heating zone or temperature control cabinet. The customer is a packaging manufacturer in Thailand using several moulds, most of them 48-cavity (48 part cavities in a single mould). When any one zone cannot heat, the whole mould has to wait for repair.
The customer reported various symptoms, such as a heater zone raising a short-to-ground alarm (Short to Ground), a control cabinet screen that would not turn on, or plastic and carbon deposits building up and obstructing flow in the runners. The customer issued work orders per job according to the symptoms, over several rounds between 2021 and 2025.
What is a Hot Runner?
A Hot Runner is the set of runners in a plastic injection mould, with heaters that keep the plastic molten from the Sprue (the point that receives plastic from the injection machine), through the Manifold (the runner plate that distributes the plastic), to the nozzle of every cavity. Each section is divided into zones, with thermocouples measuring the temperature and a temperature control cabinet controlling each one separately. If any one zone cannot heat, the mould cannot produce a full set of parts.
Requirements and constraints
This work requires finding the right root cause before replacing parts, and testing before returning the mould. The main requirements and constraints are as follows:
- There are several moulds with different codes, most of them 48-cavity, so every job has to check the problem zone on that specific mould directly.
- The same symptom may come from the temperature control cabinet, the wiring between the cabinet and the mould, or parts inside the mould, so both sides have to be checked.
- Some work is done at the customer's factory. Other work, such as Manifold cleaning, requires removing the runner assembly from the mould and sending the parts out.
- The mould must pass testing before returning to the production line. Most jobs close with a service report, and some have an acceptance document for the customer's representative to sign.
- The work is on a per-job basis under purchase orders, not an annual maintenance contract.
Why check both the control cabinet and the mould before repairing?
Because the symptom shown on the control cabinet's screen does not tell you where the root cause is. A zone reporting a short circuit may be caused by the Back Plane (the main circuit board into which each zone's control card plugs), the wiring in the cabinet or the heater wire in the mould. If parts are replaced before finding the root cause, the same symptom may return. Fault-fixing work in this case therefore followed the checking sequence below.
- 1
Receive the fault report
Record the zone raising the alarm and the symptoms found, such as a short circuit to ground, a control cabinet screen that will not turn on, or plastic not flowing freely because of deposits in the runners.
- 2
Check the temperature control cabinet side
Open the cabinet and check the Back Plane, the MCU board (Microcontroller Unit, the cabinet's main processing board) and the wiring from the cabinet to the mould for short circuits or loose points.
- 3
Check the mould side
Check the heaters, thermocouples and wiring of the problem zone, measure the heater resistance, and see whether any wire is touching metal parts of the mould.
- 4
Repair or replace parts
Repair damaged wires and replace fuses, heaters, thermocouples, the Back Plane or Nozzle Housings (nozzle casings) according to the findings. If there are deposits, the Manifold and Cross Manifold are removed for Thermal Cleaning, then reassembled.
- 5
Test before return
Test the mould's operation and carry out a Heat-up Test to confirm that every zone heats normally, before returning the mould to the production line.
- 6
Send the service report
Summarise the symptoms, what was fixed, the cause when one was found and recommendations in a service report, which the production team keeps as part of the mould's history.
We take on work under the customer's purchase orders and coordinate repairs with partner technicians specialising in Hot Runner systems. Heater short circuit fixes, Back Plane replacement and Nozzle Housing replacement are done at the customer's factory. For Manifold cleaning and Cross Manifold repair, the customer sends the parts to us, then takes them back for reassembly.
Deliverables
What is delivered in each round is the repair work under the purchase order, together with a service report or job closure documents. The table below shows the work backed by job closure documents.
Work with job closure documents
| Year | Symptom / job | Work done |
|---|---|---|
| 2021 | Temperature control cabinet calibration | Calibration of 6 control cabinets and replacement of the mould's Hot Runner parts |
| 2024 | Mould control cabinet screen will not turn on | Found a problem on the MCU board, repaired the circuit and tested on the production line. 6-month repair warranty |
| 2024 | Plastic and carbon deposits in the runners | Removed the Manifold and Cross Manifold (runner plates that distribute plastic to each cavity's nozzle) for thermal cleaning, replaced some Nozzle Housings and Front Rings (ring parts in the nozzle assembly), then reassembled |
| 2024–2025 | Cross Manifold short circuit alarm | Checked the heaters and rewired, replaced the Sprue heater and thermocouple, then carried out a heat-up test |
| 2025 | Control cabinet Back Plane short circuit | Found the root cause to be a loose wire-fastening screw; replaced the Back Plane, re-tightened the wires, then carried out a heat-up test with the mould |
| 2025 | Zones 26 and 44 short-circuited to ground | Found a heater wire damaged during installation of the Male Insert (the male part of the mould), which then touched the Manifold plate; repaired the wire, replaced the fuse, then tested the mould |
| 2025 | Replacement of the full Nozzle Housing set | Replaced all 48 Nozzle Housings along with the Sprue heater; after testing, the mould returned to production |
Results confirmed by service reports
In 2025, after all 48 Nozzle Housings were replaced, the 48-cavity mould returned to production, and the service report states that every zone could heat. On-site repair work covered by 2025 service reports included a Heat-up Test before return.
The work on zones 26 and 44 has an acceptance document (Exit Criteria Checklist) signed by the customer's representative. The Manifold cleaning report states that plastic and carbon deposits were fully removed. This case has no business metrics such as reduced machine downtime, so we report only results backed by documents.
This packaging manufacturer issued us Hot Runner maintenance work orders over several rounds between 2021 and 2025.
What we learned
The key principles of Hot Runner repair are to find the root cause before replacing parts, to take care with heater wires during disassembly and reassembly, and to close the job with a test on the actual mould.
- Find the root cause before replacing parts. The same short circuit symptom can come from several points. In this work, on one occasion the root cause was a loose wire-fastening screw in the cabinet; on another, the control cabinet had no problem but a heater wire in the mould was damaged.
- Mould disassembly and reassembly is a risk point for heater wires. A heater wire damaged during part installation that then touches the Manifold plate can cause a zone to short-circuit to ground, so the wire routing should be checked every time before turning on the heat.
- Close the job with a test on the actual mould and record the cause. A heat-up test confirms that every zone is working again, while a service report recording the cause helps the production team know where to take care in the next round.
How this approach can apply to your factory
If your factory uses Hot Runner plastic injection moulds, you can use the same checking sequence as this case: check the temperature control cabinet and wiring, then the heaters and thermocouples in the mould, before repairing and carrying out a heat-up test. What needs adjusting is the detail of each mould and control cabinet model.
Reusable parts and parts that need adapting
| Part of the work | Reusable | Needs adapting when |
|---|---|---|
| Checking sequence | Check the control cabinet and wiring, then the heaters and thermocouples in the mould | A different model of control cabinet or Hot Runner system needs that model's manual and reference values |
| Work location | Separate work that can be repaired on site from work that requires removing parts | The production line cannot stop for long, so plan which work is done on site and which requires removing parts |
| Testing before return | Mould function test and Heat-up Test on every zone | If the number of cavities and zones differs from this case, the test items must be redefined. |
| Job close-out documents | A service report stating the symptoms, what was corrected and the cause | If your factory uses its own work acceptance form, the items must be agreed before work starts. |
| System cleaning interval | Scheduled Manifold cleaning to reduce residue build-up. The Manifold cleaning report in this case recommends every 6–12 months. | If your usage differs from this case, the cleaning interval must be set according to actual usage. |
- Prepare mould and control cabinet details, such as the mould code, number of cavities, control cabinet model and the zones raising alarms, to assess which spare parts need to be prepared.
- Keep the service report from each job with the mould's history, to see whether the same symptom recurs in the same zone.
Read more
- System care and maintenance service
- Case: mould shot counting and maintenance cycle alerts (Mold PM)
- Case: totalling plastic injection machine shots per Part No.
- InCBM: monitoring machine condition from real data
- Article: Predictive Maintenance starting from the Shot Count of plastic injection moulding machines
Technology used
Frequently Asked Questions
Can repairs be done at the customer's factory, or does the mould have to be sent in for repair?
Both are possible. In this case, the heater short circuit repair, Back Plane replacement and Nozzle Housing replacement were done at the customer's factory, while for the Manifold cleaning and Cross Manifold repair, the customer sent the parts to us.
What can cause a heater short circuit to ground (Short to Ground)?
It can occur at several points, both in the control cabinet and in the mould. In the work on zones 26 and 44 in this case, the Back Plane and the wiring from the control cabinet were checked first, but no problem was found. The mould side was then checked, and it was found that a heater wire had been damaged during installation of mould components and had come into contact with the Manifold plate. Once the wire was repaired and the fuse replaced, the mould passed testing.
How often should a Hot Runner system be cleaned?
It depends on usage. The Manifold cleaning report in this case recommends cleaning every 6–12 months, so that plastic and carbon residue does not build up to the point of obstructing flow, and inspecting the nozzles and Manifold periodically.
What documents do we receive after the repair is complete?
Most of the work in this case came with a Service Report stating the symptoms, what was corrected, the cause when one was identified, and recommendations. Some jobs also had a work acceptance document (Exit Criteria Checklist) for the customer's representative to sign.
How are service fees calculated?
There is no standard price. It depends on the symptoms, the spare parts that need replacing and the work location. You can request a quotation by telling us the mould model, the control cabinet and the symptoms found.