





Camera system for colour shade sorting and black spot inspection, for a recycled paper sheet manufacturer
This camera system compares the colour shade of recycled paper sheets against a prototype workpiece (Master), inspects the sheet surface for black spots and plastic marks, and then shows an OK or NG result for each sheet. We built a test rig and a prototype program, and tested them with 2 groups of sample workpieces from a recycled paper sheet manufacturer in 2016.
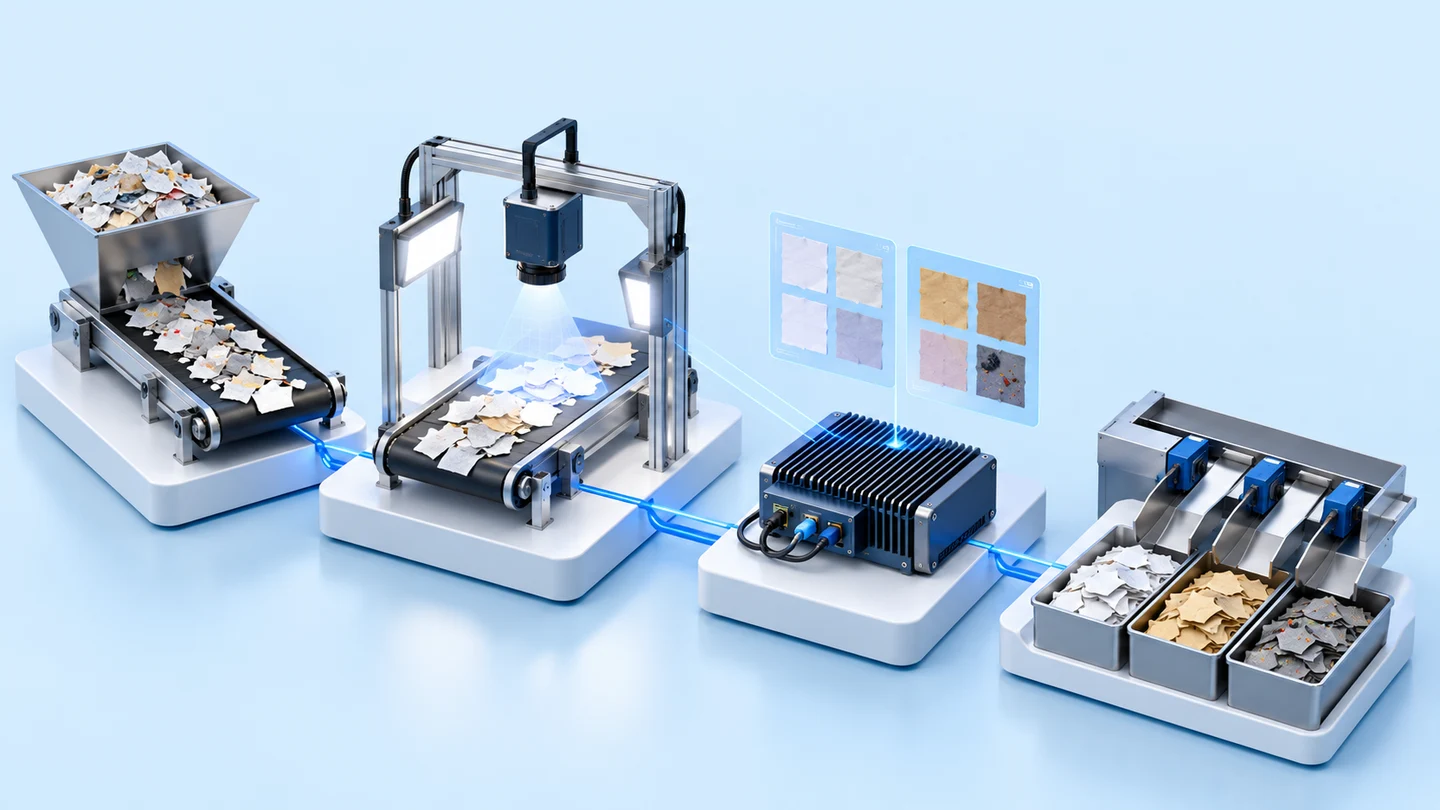
- Bar lightBrightness controlled by Lighting Control
- Cube 5MP cameraCaptures images of paper sheets on the test cabinet
- Medusa processing unitCompares shade with Master + inspects black spots
- OK / NG resultThe sorting report is a part designed for the full system
- Industry
- General manufacturing
- Year
- 2016
- Scope of work
- Camera system for colour shade sorting and cleanliness inspection of recycled paper sheets · Input: images from a Cube 5MP camera on a test cabinet, under 2 bar lights with brightness controlled by a Lighting Control unit · Processing: a Medusa processing unit compares each sheet's colour shade against the group's prototype workpiece (Master), and checks the number and size of black spots and plastic marks · Output: OK (pass) in green or NG (fail) in red · Software: prototype program with Login, Process and Setting pages · Designed for the full system: reports sorting good and defective work, Manual and Automatic modes · What we built and tested: a test rig and a prototype program, tested for colour shade comparison and for black spot and plastic mark inspection with 2 groups of the customer's sample workpieces in 2016, with a test report
Summary
- This camera system sorts colour shades and inspects black spots on recycled paper sheets. We built a test rig and a prototype program, then tested them with 2 groups of the customer's sample workpieces in 2016.
- The system checks 2 things: the sheet's colour shade (brightness) against the prototype workpiece (Master), and the sheet's cleanliness based on the number and size of black spots and plastic marks.
- The test rig uses a Cube 5MP camera, 2 bar lights with brightness controlled by a Lighting Control unit, and a Medusa processing unit.
- In the test, the program reported that 1 sheet's shade did not match the group's Master, and it found many plastic marks and black spots on sheets in the same group.
- The design target for inspection time is about 3 seconds per sheet in Manual mode and about 1 second per sheet in Automatic mode, and this must be measured again against the actual production line speed.
The on-site brief
The recycled paper sheet manufacturer wanted to separate sheets with unsuitable brightness (shade) from good ones, and to assess sheet cleanliness from the number and size of black spots or foreign matter. The question before investing was whether a camera could do these 2 tasks on real workpieces.
What we did
We set up a test rig with a Cube 5MP camera, 2 bar lights with brightness controlled by a Lighting Control unit, and a Medusa processing unit, then wrote a prototype program that compares each sheet's colour shade against the prototype workpiece and checks the number and size of black spots and plastic marks. The program shows OK (pass) in green and NG (fail) in red.
Test results with real workpieces
In the test with the customer's 2 groups of sample workpieces, the program reported that 1 sheet's shade did not match the group's prototype workpiece, and it found many plastic marks and black spots on sheets in the same group. The design target for inspection time is about 3 seconds per sheet in Manual mode and about 1 second per sheet in Automatic mode, and this must be measured again against the actual production line speed.
How the brief came about
This system uses a camera to sort recycled paper sheets by colour shade and to assess sheet cleanliness from black spots on the surface. The task was to prove, before investing, that a camera could do these 2 tasks on real workpieces. The recycled paper sheet manufacturer wanted to separate sheets with unsuitable brightness from good ones, and to measure cleanliness from the number and size of black spots or foreign matter on the paper surface.
Colour and cleanliness are what the end customer sees immediately on receiving the paper sheets. When the sorting criteria depend on an inspector's eye, it is hard to state as a repeatable criterion which sheets pass and which do not. So we began by testing a prototype with the customer's sample workpieces in 2016.
Requirements and constraints
The prototype had to meet the customer's 2 requirements and be tested with sample workpieces on a test cabinet. The main requirements and constraints are as follows.
- Inspect the sheet's brightness (colour shade) to separate sheets with suitable brightness from unsuitable ones
- Assess sheet cleanliness from the number and size of black spots and plastic marks on the surface
- Use the customer's sample workpieces in 2 groups, each group with its own prototype workpiece (Master)
- Test on a test cabinet with controllable lighting; lighting conditions and the installation position in the factory must be surveyed separately before installation
How does this system sort colour shades and inspect black spots?
This prototype captures an image of each paper sheet, one at a time, under brightness-controlled lighting, then uses image processing to compare the sheet's colour shade against the group's prototype workpiece (Master) and to count black spots and plastic marks on the surface. The result for each sheet is shown as OK (pass) or NG (fail).
- 1
Control the lighting
2 bar lights illuminate from either side of the lens and workpiece. The Lighting Control unit adjusts the light brightness to the set value.
- 2
Capture images of the paper sheet
A Cube 5MP camera mounted on the test cabinet captures images of the recycled paper sheet placed below.
- 3
Set up and select the prototype workpiece
The user sets sharpness, colour tone and brightness on the program's Setting page, then assigns a Master for each workpiece group as the reference.
- 4
Compare shades and inspect black spots
The Medusa processing unit compares the sheet's shade with the Master and shows OK in green or NG in red, and also checks the number and size of black spots and plastic marks on the sheet.
What is a prototype workpiece (Master)?
A prototype workpiece is the sheet used as the reference for shade comparison. A sheet whose shade matches the group's Master gets an OK result, and a sheet whose shade differs gets an NG result.
We chose to compare against each group's Master because the customer's task was to separate sheets that differ from that group's reference sheet. In colour shade comparison, the brightness the camera sees also depends on the lighting, so the test rig controls the bar lights with a Lighting Control unit.
What we built and tested
We built a test rig and a prototype program, then tested them with the customer's sample workpieces. The details are as follows.
- Test rig: Cube 5MP camera on a test cabinet, 2 bar lights with a Lighting Control unit, and a Medusa processing unit
- Prototype program with Login, Process and Setting pages
- Testing with the customer's sample workpieces, covering both colour shade comparison and inspection of black spots and plastic marks
- Test report and the design of the full system: a report sorting good and defective work, and Manual and Automatic modes
Details of test results on real workpieces
In the test with the customer's 2 groups of sample workpieces, the program reported that 1 sheet's shade did not match the group's Master, while the other sheets were reported as matching their own group's Master. The cleanliness inspection found many plastic marks and black spots on sheets in the same group. This result comes from a test cabinet with controlled lighting. The documents do not separately confirm that the sheet's shade was actually wrong, and results on a production line must be measured again under on-site lighting.
The design target for inspection time is about 3 seconds per sheet in Manual mode (the user controls the inspection) and about 1 second per sheet in Automatic mode (the system inspects automatically). Both values must be measured again against the actual production line speed.
Scope of the test results
This result comes from 2 groups of sample workpieces on a test cabinet with controllable lighting. Before installation on a production line, the environment and installation position in the factory must be surveyed, and the lighting must be tested again with real workpieces.
What we learned
This work gives 3 principles for camera-based colour shade and cleanliness inspection of flat sheet workpieces.
- Control the light before comparing colour. The brightness the camera sees also depends on the lighting, so a shade comparison can be trusted when the lighting is stable and adjustable, not merely when the camera has high resolution.
- Set criteria from an agreed reference workpiece. Each workpiece group should have its own Master, and before actual use the Master should be a sheet the customer accepts, so that an OK or NG result means the same thing every time.
- A result in a test cabinet is not yet a result on a production line. Before actual installation, the lighting conditions and installation position in the factory must be surveyed, and inspection time per sheet must be measured against the actual line speed.
How this approach can apply to your factory
If your factory needs to sort flat sheet workpieces by colour shade or brightness, or wants cleanliness criteria based on black spots instead of visual judgement, you can use the same approach as this prototype: control the lighting, compare against each group's Master, and count spots on the surface. What needs adjusting is the lighting and the decision criteria, when your workpiece or site differs from this work.
Reusable parts and parts that need adapting
| System part | Reusable | Needs adapting when |
|---|---|---|
| Lighting and camera | Illumination with brightness-controllable bar lights, and a camera looking down at the workpiece | If the workpiece differs in colour or surface, the lighting must be tested again with real workpieces, because different surfaces reflect light differently. |
| Colour shade comparison | Comparing each sheet with the group's Master and showing an OK / NG result | If your factory does not yet have a Master accepted by the customer, a reference workpiece must be agreed first. |
| Cleanliness inspection | Counting and measuring the size of black spots and marks on the surface | What spot size and what quantity count as a fail must be defined anew. |
| Installation | A test step with sample workpieces on a test cabinet before investing in the full system | To install on an actual production line, lighting conditions, installation position and line speed must be surveyed first. |
- Prepare sample workpieces, both good and defective sheets, along with a Master for each group, for testing and setting criteria
- Choose between a mode the user controls and an automatic mode, then compare inspection time per sheet with the production line speed
- Plan how sorting results will be passed on, for example using a report for people to remove sheets, or connecting to the production line's sorting mechanism
Read more
- Case: Prototype program for camera-based workpiece colour shade inspection (IKS2 Shading)
- Case: Camera system for counting dark spots on white powder (Spot Counter)
- Case: Camera system for lotion bottle cap orientation inspection
- Article on choosing an AI inspection camera: off-the-shelf Task Cam or custom-built Machine Vision
- Custom inspection and control system development service
- AI / IoT consulting and system design service
Technology used
Frequently Asked Questions
How does the system know which sheet has the wrong shade?
The system compares the image of each sheet with the group's preset prototype workpiece (Master), with images captured under brightness-controlled lighting. A sheet whose shade matches the Master shows OK (pass) in green, and a sheet that does not match shows NG (fail) in red.
To what extent can sheet cleanliness be inspected?
In the test, the program checked the number and size of black spots and plastic marks on the sheets, and found many plastic marks and black spots on sheets in one group. The criteria for which sheets pass must be defined jointly with the factory from real workpieces.
How fast can it inspect per sheet?
The design target is about 3 seconds per sheet in Manual mode and about 1 second per sheet in Automatic mode. Both values must be measured again against the actual production line speed before use.
What does the factory need to prepare before testing?
Prepare sample workpieces, both good and defective sheets, along with a customer-accepted Master for each group; define what black spot size and quantity count as a fail; and provide the production line speed and the position where the camera will be installed.
If I want a system like this, how much does it cost?
There is no standard price. The price depends on the sample workpieces, the sorting criteria, the speed of the production line and the site conditions. Please contact us to request a quotation.


